
Onx Control Codesys Türkiye
Resmi Sistem Partneri
CODESYS ile Donanımdan Bağımsız
Makine Kontrolü.
ONX Control; CODESYS nedir sorusunun Türkiye'deki en yetkin cevap merkezi ve resmi System Partner ağı içinde yer alan, 20 yılı aşkın saha tecrübesine sahip otomasyon mühendisliği merkezidir. İşletmenizin veya makinenizin ihtiyaç duyduğu tüm CODESYS altyapısı için lisanslama, eğitim ve sistem entegrasyonu hizmetlerini tek çatı altında birleştiriyoruz...
Sistem Geliştirme Teknolojileri
Endüstriyel PC, Panel PC ve Linux/Windows tabanlı hedefleriniz için SoftPLC, Motion ve HMI bileşenleri.
PC Tabanlı Otomasyon ve CODESYS Mimarisi Nedir?
CODESYS Engineering
IEC 61131-3 tabanlı mühendislik ortamı; PLC projesi, kütüphane, debug ve ekip standardizasyonu için ana çalışma platformu.
- ST, LD, FBD, SFC ve CFC
- Online debug ve izleme
- Kütüphane ve proje standardı
CODESYS Runtime
Endüstriyel PC, panel PC, Linux/Windows tabanlı hedefler ve gömülü cihazlar için SoftPLC çalışma zamanı.
- SoftPLC kontrol çekirdeği
- Donanımdan bağımsız yapı
- Saha ve makine kontrolü
CODESYS Visualization
Makine arayüzleri, WebVisu, reçete, alarm, trend ve operatör ekranlarını aynı proje disipliniyle yönetir.
- HMI ve WebVisu
- Alarm, trend, reçete
- Tarayıcı ve panel desteği
CODESYS Motion CNC Robotics
Servo eksenler, elektronik kam, senkron hareket, interpolasyon, CNC yol kontrolü ve robot kinematiği için entegre motion katmanı.
- PLC + motion tek projede
- CNC yol kontrolü
- Robot kinematiği entegrasyonu
CODESYS Fieldbus & Communication
EtherCAT, PROFINET, CANopen, Modbus ve endüstriyel haberleşme protokollerini mühendislik ortamına bağlayan saha katmanı.
- Sürücü ve I/O entegrasyonu
- Endüstriyel ağ topolojileri
- IT/OT bağlantıları
CODESYS Automation Server
CODESYS tabanlı kontrol sistemlerinin merkezi erişim, bakım, güncelleme ve yaşam döngüsü yönetimi için bulut destekli katman.
- Merkezi cihaz yönetimi
- Uzaktan bakım
- Proje ve kontrolör takibi
CODESYS Safety
Fonksiyonel güvenlik uygulamalarını otomasyon mimarisiyle uyumlu ve sürdürülebilir bir yapıda ele almayı destekler.
- Güvenlik mantığı
- Makine güvenliği
- Standartlaştırılmış yapı
CODESYS Store & Ecosystem
Eklentiler, kütüphaneler, SoftPLC hedefleri ve örnek projelerle CODESYS ekosistemini genişleten uygulama mağazası.
- Eklentiler ve kütüphaneler
- Örnek projeler
- Cihaz açıklama dosyaları
Codesys RTE/Motion Bazlı Projelerimizden Örnekler

What is G-code? CNC Programming Explained, Line by Line
What is G-code, and how does a CNC controller read it? This video explains the language of CNC machines: how a block is built (N, G, M, X/Y/Z, I/J/K, F, S, T and comments), modal commands, G0 rapid vs G1 linear feed, G2/G3 arcs with I/J or R and the G17/G18/G19 planes, G20/G21 units, G90 absolute vs G91 incremental positioning, G54–G59 work offsets and G53, tool length (G43 H) and cutter radius compensation (G41/G42/G40 with D), the common M codes (M3/M4/M5, M6, M8/M9, M0/M1, M30), a complete part program line by line, how CAM and the post processor write G-code, and how the controller runs it with an interpreter, look-ahead and an interpolator. Free DXF to G-code converter (writes X CNC G-code, shows the toolpath in 3D and simulates the motion, in your browser): https://www.onxcontrol.com/en/products/x-cnc/dxf-to-gcode-converter Chapters 0:00 Intro 0:29 What G-code is 1:10 Anatomy of a block 1:44 Modal commands 2:12 G0 and G1 2:43 Arcs: G2 and G3 3:12 Units and positioning 3:43 Work coordinates 4:11 Tool compensation 4:44 M codes, S and T 5:11 A program, line by line 6:16 CAM and post processors 6:45 How the controller runs it 7:46 Free DXF to G-code converter In short - A G-code program is plain text (RS-274 / ISO 6983). Each line is a block; each word is a letter plus a number. - Modal codes (G0/G1, F, G90…) stay active until replaced by a code from the same group; G4 dwell works only in its own block. - G0 = rapid positioning (path may not be straight), G1 = straight line at feed, G2/G3 = clockwise/counter-clockwise arc (I/J = start point to centre, or R). - G17/G18/G19 = XY/ZX/YZ plane, G21/G20 = mm/inch, G90/G91 = absolute/incremental. - G54–G59 = work offsets (machine zero → part zero), G53 = machine coordinates. - G43 H = tool length offset; G41/G42 D = cutter radius compensation left/right, G40 = off. - M3/M4/M5 spindle, T… M6 tool change, M8/M9 coolant, M0/M1 stop, M30 end and rewind. - Every controller has a dialect: a post processor adapts the CAM toolpath; check your controller's manual. X CNC Library: https://www.onxcontrol.com/en/products/x-cnc CNC router control system: https://www.onxcontrol.com/en/solutions/cnc-router-control-system Also in this series: What is CNC?: https://youtu.be/8vnFXo1jhng Servo Motor vs Stepper Motor: https://youtu.be/sH2kzHz0i5g Encoder Explained: https://youtu.be/4UoyIwBAxug PID Controller Explained: https://youtu.be/KKCBE6LhDEM VFD Explained: https://youtu.be/SbVYrV1-jBM ONX Control, Istanbul: motion control and PC-based automation for machine builders. CODESYS System Partner. #gcode #cnc #cncprogramming

What is CNC? How CNC Machines Work, from CAD to Servo Motion
What is CNC, and how does a CNC machine turn a drawing into a part? This video explains Computer Numerical Control from the ground up: the step from NC to CNC, the full control chain (CAD, CAM, G-code, CNC controller, interpolator, servo drive, motor, axis), how interpolation turns a path into position targets every cycle, the closed loop with encoder feedback and following error, 3-, 4- and 5-axis machines and RTCP, the main machine types (milling, lathe, router, plasma, laser, waterjet and more), the parts of a CNC machine tool, resolution vs repeatability vs accuracy, and why PC-based CNC needs real-time control and low jitter. Free DXF to G-code converter (toolpath in 3D and a motion simulation, in your browser): https://www.onxcontrol.com/en/products/x-cnc/dxf-to-gcode-converter Chapters 0:00 Intro 0:30 What CNC means 0:56 From NC to CNC 1:39 The control chain 2:16 Interpolation 2:56 Closed loop 3:23 Axes: 3, 4 and 5 3:57 Machine types 4:48 Inside a CNC machine 5:17 Accuracy and repeatability 5:47 PC-based CNC and real time 6:57 About ONX Control In short - CNC = Computer Numerical Control: moves are written as numbers (G-code) and a controller drives a motor on every axis. - Control chain: CAD (geometry) → CAM (tools, path, feeds) → G-code → CNC controller (reads and plans ahead) → interpolator (a position target for every axis in every cycle) → servo drive → motor → ball screw or rack → axis. - Interpolation: at 6 m/min the tool moves 0.1 mm per 1 ms cycle; speed ramps within each axis's velocity, acceleration and jerk limits. - Closed loop: the drive compares the target with the encoder position; position, speed and current loops correct the following error. An open-loop stepper never knows about lost steps. - Axes: X, Y, Z; a 4th rotary axis (A about X); 5 axes tilt the tool, and RTCP keeps the tool tip on the path. - Resolution = smallest step; repeatability = returning to the same point; accuracy = reaching the true position. Compensation, warm-up and good mechanics close the gap. - PC-based CNC: the operator screen can wait, the motion cannot. EtherCAT sends targets to all drives every cycle; jitter must stay small. X CNC Library: https://www.onxcontrol.com/en/products/x-cnc CNC router control system: https://www.onxcontrol.com/en/solutions/cnc-router-control-system CNC metal cutting: https://www.onxcontrol.com/en/solutions/cnc-metal-cutting Also in this series: Servo Motor vs Stepper Motor: https://youtu.be/sH2kzHz0i5g Encoder Explained: https://youtu.be/4UoyIwBAxug PID Controller Explained: https://youtu.be/KKCBE6LhDEM VFD Explained: https://youtu.be/SbVYrV1-jBM Cable Sizing Explained: https://youtu.be/JmdxoNshV_4 DC to AC Motor Conversion: https://youtu.be/3DGPoq0xKPQ ONX Control, Istanbul: motion control and PC-based automation for machine builders. CODESYS System Partner. #cnc #cncmachine #motioncontrol

Encoder Explained: Incremental vs Absolute, Resolution and Signals
How does an encoder work, and which one should you choose? This video explains optical and magnetic encoders, incremental A/B quadrature with the Z index, why incremental axes must home after a power cut, absolute single-turn and multi-turn encoders with Gray code, what 17, 20 and 23 bit resolution really means, the common signals and protocols (TTL/RS-422, HTL, SinCos, SSI, EnDat, Hiperface, BiSS, resolver), and when a machine needs a measuring wheel as well as the motor encoder. Free Estun servo configurator (motor, drive, encoder and cables matched, no sign-up): https://www.onxcontrol.com/en/products/estun/servo-configurator Chapters 0:00 Intro 0:34 How an encoder works 1:05 Incremental encoders 2:01 Absolute encoders 2:41 Resolution 3:37 Signals and protocols 4:29 Motor encoder vs machine encoder 5:07 How to choose 5:52 About ONX Control In short - Incremental: A and B are 90° apart (quadrature); the edge order gives the direction; Z gives one index pulse per revolution. Counting every edge gives 4 counts per line: 2,500 lines → 10,000 counts per revolution. The count is lost at power-off, so the axis must home (home switch, then Z). - Absolute: a unique code (usually Gray code) at every position, known at power-up. Single-turn knows the position within one revolution; multi-turn also counts revolutions with gears or a battery-backed counter. - Resolution: 17 bit = 131,072, 20 bit = 1,048,576, 23 bit = 8,388,608 counts per revolution (364 / 2,913 / 23,302 per degree). At 1 rpm a 17-bit encoder moves about 2 counts per millisecond, a 23-bit one about 140, so the speed signal and low-speed motion are much smoother. Resolution is not accuracy. - Signals: TTL/RS-422 differential (long cables), HTL 10–30 V (PLC counters, measuring wheels), SinCos (interpolated), serial SSI/EnDat/Hiperface/BiSS (absolute position as data, diagnostics, electronic nameplate), resolver (heat and vibration). - Motor encoder vs measuring wheel: feed roll slip and wear make the motor encoder over-report travel; precise lines use the motor encoder for the loop and a measuring wheel for length correction. - How to choose: position at power-up → absolute multi-turn; slow smooth motion or CNC → 20–23 bit; match the drive's protocol; differential/serial for long cables, resolver for harsh conditions; mount and align it well. Servo systems: https://www.onxcontrol.com/en/products/servo-systems Estun EM3 servo motors: https://www.onxcontrol.com/en/products/estun/em3 HPB PM/PMA servo motors: https://www.onxcontrol.com/en/products/hpb/pm-pma Unimotor hd: https://www.onxcontrol.com/en/products/control-techniques/unimotor-hd Unidrive M700: https://www.onxcontrol.com/en/products/control-techniques/unidrive-m700 Free motor sizing calculator: https://www.onxcontrol.com/en/calculators/motor-sizing Also in this series: Servo Motor vs Stepper Motor: https://youtu.be/sH2kzHz0i5g VFD Explained: https://youtu.be/SbVYrV1-jBM PID Controller Explained: https://youtu.be/KKCBE6LhDEM Cable Sizing Explained: https://youtu.be/JmdxoNshV_4 DC to AC Motor Conversion: https://youtu.be/3DGPoq0xKPQ ONX Control, Istanbul: motion control and PC-based automation for machine builders. CODESYS System Partner. #encoder #servomotor #motioncontrol

DC to AC Motor Conversion: Retrofit, Vector Control and Payback
Should you convert an old DC motor drive to AC, or keep the DC motor and renew the drive? This video explains why DC motors were the standard for variable speed, how a closed-loop vector drive makes an AC induction motor behave like a DC motor, what to check before a retrofit, and how to work out the payback, with a worked example. Free DC to AC retrofit ROI calculator (payback, 5-year return, CO₂, no sign-up): https://www.onxcontrol.com/en/calculators/dc-to-ac-retrofit-roi Chapters 0:00 Intro 0:34 How a DC motor is controlled 1:18 Where DC costs you 2:00 How an AC drive replaces DC 3:08 Before you convert 4:00 Braking and regeneration 4:35 Drive and installation 5:08 Keep DC or convert? 5:40 Does it pay back? 6:41 About ONX Control In short - DC motor: torque T = k·Φ·I_a, speed n ≈ U_a/(k·Φ). A thyristor converter sets the armature voltage; above base speed the field is weakened for constant power. - Costs of DC: brush and commutator wear, a power factor that falls with speed on thyristor drives, ageing drives and spare parts, commutator sparks. - Vector control splits the stator current into I_d (flux, like the DC field current) and I_q (torque, like the armature current): full torque at zero speed, constant torque up to base speed, constant power above it, limited by the AC motor's breakdown torque. - Before you convert: match torque at base speed and power at top speed, forced cooling for low-speed high-torque duty, mechanical fit, encoder instead of an analog tacho. - Braking: a four-quadrant DC drive regenerates to the grid; a standard AC drive with a diode rectifier cannot, so plan a braking resistor or an active front end. - Drive and installation: size by current and duty, shielded motor cable, insulated bearing on larger motors, analog reference or fieldbus. - Keep DC when the motor is healthy and only the drive is obsolete; convert when the motor needs a rewind, maintenance and downtime cost too much, or you want one platform. - Worked example (calculator defaults): 90 kW shaft, 84 % vs 94 % efficiency, 6,600 h/year at €0.14/kWh → €10,532 energy; €35,532 total annual gain; €39,000 net investment → 13.2 months payback. Energy is under a third of the gain. Products in the video Leroy-Somer CPLS motors: https://www.onxcontrol.com/en/products/leroy-somer/cpls Unidrive M700: https://www.onxcontrol.com/en/products/control-techniques/unidrive-m700 Unidrive M000 modular drives: https://www.onxcontrol.com/en/products/control-techniques/unidrive-m000 Mentor MP DC drive: https://www.onxcontrol.com/en/products/control-techniques/mentor-mp Also in this series: VFD Explained: https://youtu.be/SbVYrV1-jBM Servo Motor vs Stepper Motor: https://youtu.be/sH2kzHz0i5g PID Controller Explained: https://youtu.be/KKCBE6LhDEM Cable Sizing Explained: https://youtu.be/JmdxoNshV_4 ONX Control, Istanbul: official distributor and system integrator for Nidec Control Techniques drives. Motion control and PC-based automation for machine builders. #dcmotor #retrofit #vfd

Cable Sizing Explained: Voltage Drop, Ampacity and Short Circuit
How do you size a cable properly? Ampacity tables are only the first of five checks. Using a real example, a 22 kW motor 80 m from the panel, this video walks through every check in IEC 60364: current-carrying capacity with installation methods and correction factors, overload protection, voltage drop (also during motor starting), short-circuit withstand and the earth fault loop, plus harmonics in the neutral. Free cable size calculator (all five checks, 9 IEC installation methods, PDF report, no sign-up): https://www.onxcontrol.com/en/calculators/cable-sizing Chapters 0:00 Intro 0:27 The five checks 0:54 1. Current-carrying capacity 1:22 Correction factors 1:50 2. Overload protection 2:26 3. Voltage drop 3:12 4. Short-circuit withstand 3:58 5. Earth fault loop 4:41 Harmonics and the neutral 5:05 Worked example 5:20 Free calculator In short - Current-carrying capacity: the table value for the installation method (A1 to G), multiplied by correction factors for ambient or ground temperature, grouping, soil resistivity and harmonics, must cover the load. - Overload protection: design current ≤ breaker rating ≤ cable capacity (I_B ≤ I_n ≤ I_z), and for fuses I₂ ≤ 1.45·I_z. - Voltage drop: u = b·(R·cos φ + X·sin φ)·I·L. IEC 60364-5-52 Annex G recommends 3 % for lighting and 5 % for other loads (public LV supply). Check motor starting too. - Short circuit: k²·S² ≥ I²·t (k = 115 copper PVC, 143 copper XLPE). - Earth fault loop (TN): Z_s·I_a ≤ U₀ sets a maximum cable length; a type C breaker needs 10·I_n to trip instantly. - Example: 22 kW motor at 80 m: current alone says 6 mm², but the 50 A breaker and the fault loop need 10 mm². AC drives and motors: https://www.onxcontrol.com/en/products/ac-drives-and-motors More free engineering calculators: https://www.onxcontrol.com/en/calculators Also in this series: Servo Motor vs Stepper Motor: https://youtu.be/sH2kzHz0i5g VFD Explained: https://youtu.be/SbVYrV1-jBM PID Controller Explained: https://youtu.be/KKCBE6LhDEM ONX Control, Istanbul: motion control and PC-based automation for machine builders. CODESYS System Partner. #cablesizing #voltagedrop #electricalengineering

PID Controller Explained: P, I, D, Tuning and Winder Tension
What do the P, the I and the D in a PID controller actually do? One simulated step response shows all three, then: how to tune a loop without guesswork, integral windup, and how PID works together with feed-forward to hold tension on a real winder. Winder and unwinder tension control (diameter calculation, dancer or load cell, taper tension): https://www.onxcontrol.com/en/solutions/winder-unwinder-tension-control Chapters 0:00 Intro 0:35 The feedback loop 0:59 P, I and D 2:06 How to tune a PID loop 2:44 Winder tension: feed-forward plus PID 3:22 Dancer or load cell? 3:51 On a real machine 4:13 About ONX Control In short - A PID controller compares the setpoint with the measured process variable and turns the error into an output: u = Kp·e + Ki·∫e dt + Kd·de/dt. - P reacts immediately but leaves an offset; more gain is faster but overshoots. I removes the offset but adds overshoot, and needs anti-windup. D damps the overshoot but amplifies noise, so it is filtered; many real loops run as PI. - Tuning: step test (process gain, dead time, time constant), start with P, add I, add D only if needed, set limits and anti-windup, log the trends, use gain scheduling if the process changes. - Winder tension: motor torque T = F·r / (i·η). As the roll grows, torque rises and speed falls. Feed-forward from the calculated diameter does most of the work; the PID trims the rest with a dancer or a load cell. PID process control (temperature, pressure, flow, level): https://www.onxcontrol.com/en/solutions/pid-process-control Slitting line automation: https://www.onxcontrol.com/en/solutions/slitting-line-automation More free engineering calculators: https://www.onxcontrol.com/en/calculators Also in this series: Servo Motor vs Stepper Motor: https://youtu.be/sH2kzHz0i5g VFD Explained: https://youtu.be/SbVYrV1-jBM ONX Control, Istanbul: motion control and PC-based automation for machine builders. CODESYS System Partner. #pidcontroller #pidcontrol #tensioncontrol

VFD Explained: How a Variable Frequency Drive Works
What is a VFD and how does it work? Rectifier, DC bus and inverter, pulse width modulation, control modes, energy savings on pumps and fans, braking and regeneration, and harmonics, in under six minutes. Free pump and fan energy savings calculator (VFD vs valve or damper, CO2, payback): https://www.onxcontrol.com/en/calculators/pump-fan-energy-savings Chapters 0:00 Intro 0:32 Why frequency sets the speed 1:12 Inside a VFD 2:03 Control modes 2:28 Energy savings on pumps and fans 2:59 Braking and regeneration 3:41 Harmonics and power quality 4:09 Practical tips 4:42 About ONX Control In short - Synchronous speed n = 120 x f / p. A 4-pole motor runs at 1,500 rpm on 50 Hz (1,800 rpm on 60 Hz), minus slip. A VFD changes the frequency, and the voltage with it (V/f), to change the speed. - Inside: a rectifier (AC to DC), the DC bus (around 560 V DC on a 400 V supply) and an inverter whose IGBTs build a new three-phase output with PWM. - Control modes: V/f for pumps and fans, sensorless vector for strong low-speed torque, closed-loop vector with an encoder for full torque at zero speed. - Pumps and fans: power falls with the cube of speed. At 80 % speed a fan needs about 51 % of the power. Constant-torque loads (conveyors, extruders) save only in proportion to speed. - Braking: a decelerating motor becomes a generator and raises the DC bus voltage. Use a longer ramp, a brake chopper and resistor, or a regenerative active front end (AFE). - Harmonics: diode rectifiers draw pulsed current. Chokes and filters reduce harmonics; an AFE draws nearly sinusoidal current and can regenerate. Active front end payback calculator: https://www.onxcontrol.com/en/calculators/afe-roi AC drives and motors (Control Techniques Unidrive M700, Commander C, Leroy-Somer IE3/IE4): https://www.onxcontrol.com/en/products/ac-drives-and-motors More free engineering calculators: https://www.onxcontrol.com/en/calculators Also in this series: Servo Motor vs Stepper Motor: https://youtu.be/sH2kzHz0i5g ONX Control, Istanbul: official distributor and system integrator for Nidec Control Techniques drives. Motion control and PC-based automation for machine builders. #vfd #variablefrequencydrive #acdrive

Servo Motor vs Stepper Motor: How They Work and Which One to Choose
Servo or stepper? How each motor works, where each one wins, and how to choose the right one for your machine, with a worked servo sizing example. Free servo motor sizing calculator (torque, speed, inertia ratio, matching motors, no sign-up): https://www.onxcontrol.com/en/calculators/motor-sizing Chapters 0:00 Intro 0:22 How a stepper motor works 1:40 How a servo motor works 2:27 Torque, speed and heat 2:59 Side-by-side comparison 3:29 Which one should you choose? 4:05 Servos in real machines 4:40 How to size a servo motor 5:55 About ONX Control In short - A stepper motor runs open loop: it counts pulses and assumes the shaft followed. Overload makes it miss steps, and nobody notices. - A servo motor closes the loop with an encoder (a 23-bit encoder resolves 8,388,608 positions per revolution) and three nested loops in the drive: position, velocity and current (torque). - Stepper torque is highest at standstill and falls steeply with speed. A servo delivers rated torque nearly flat up to rated speed, plus short peaks of up to about 3x for acceleration. - Choose a stepper for low speeds, light steady loads and cost-sensitive devices. Choose a servo for speed, dynamics, changing loads and synchronized axes. Worked example (from our motor sizing guide): 50 kg carriage, ball screw with 20 mm lead, 300 mm in 0.6 s. Motor speed 2,250 rpm, load inertia 8.08 kg·cm². A low-inertia 0.4 kW servo has enough torque but an inertia ratio of 33; a medium-inertia 0.75 kW motor brings it down to 4.9. Servo systems (Estun, Control Techniques, HPB): https://www.onxcontrol.com/en/products/servo-systems Motion control solutions (flying shear, rotary knife, winders, packaging): https://www.onxcontrol.com/en/solutions ONX Control, Istanbul: motion control and PC-based automation for machine builders. CODESYS System Partner. #servomotor #steppermotor #motioncontrol

Motor Boyutlandırma ve Servo Motor Seçimi: Ücretsiz Hesaplama Aracı
Servo motor seçimini ücretsiz, kayıt olmadan yapın: https://www.onxcontrol.com/hesaplamalar/motor-boyutlandirma ONX Motion Sizing eksenin tepe ve RMS torkunu, motor devrini ve atalet oranını hesaplar; ardından katalogdan uygun servo motorları (Estun, Control Techniques, Leroy-Somer, HPB) stok durumuyla birlikte önerir. Nasıl çalışır: 1. Mekanizmayı seçin: vidalı mil, kremayer, kayış/konveyör, besleme merdanesi, döner tabla, vinç, silindir ya da özel tanımlı yük 2. Yükü girin: kütle, sürtünme, hatve ya da kasnak çapı, mil ve kavrama ataleti 3. Hareketi tanımlayın: trapez, 1/3 trapez ya da S eğrisi; hareket ve bekleme süresi 4. Redüksiyonu ekleyin: kayış, dişli, zincir ya da redüktör (her kademenin oranı, ataleti ve verimi) 5. Güvenlik paylarını ve atalet oranı sınırını belirleyin (varsayılan %10 ve 10:1) Tek tıkla metrik ya da inç-pound birimler. Videodaki örnek (sayfadaki rehberde de var): 50 kg araba, Ø25 mm, 20 mm hatveli bilyalı vida; 1/3 trapez profille 0,6 s'de 300 mm. Yük ataleti 8,08 kg·cm², motor devri 2250 d/dk. 0,4 kW düşük ataletli motorun torku yeter ama atalet oranı 33; aynı ailenin 0,75 kW orta ataletli motoru oranı 4,9'a indirir. Bu eksende motoru tork değil atalet oranı belirler. Sayfada formüller, adım adım rehber ve sık sorulan sorular da var; her sonucu elle kontrol edebilirsiniz. Diğer ücretsiz mühendislik hesaplamaları: https://www.onxcontrol.com/hesaplamalar ONX Control (Oniks Kontrol Sistemleri ve Mühendislik A.Ş.), İstanbul: hareket kontrolü, otomasyon ve servo sistemler. #servomotor #otomasyon #hareketkontrol
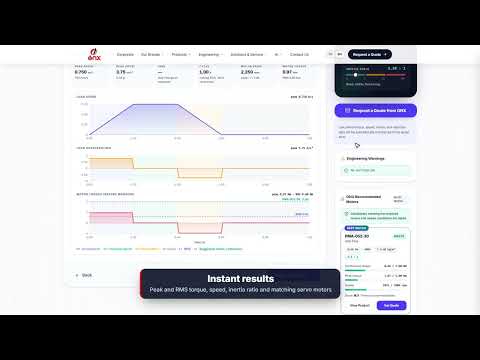
Free Servo Motor Sizing Calculator: Torque, Inertia Ratio and Motor Selection
Size a servo motor online, free, no sign-up: https://www.onxcontrol.com/en/calculators/motor-sizing ONX Motion Sizing calculates the peak and RMS torque, motor speed and inertia ratio of your axis, then proposes matching servo motors from our catalogue (Estun, Control Techniques, Leroy-Somer, HPB) with stock status. How it works: 1. Pick the mechanism: ball screw, rack and pinion, belt/conveyor, feed roll, rotary table, hoist, cylinder or a user-defined load 2. Enter the load: mass, friction, lead or pulley diameter, screw and coupling inertia 3. Define the motion: trapezoid, 1/3 trapezoid or S-curve, with move time and dwell 4. Add the reduction chain: belt, gears, chain or a gearbox (ratio, inertia and efficiency of each stage) 5. Set safety margins and the inertia-ratio limit (10 % and 10:1 by default) Metric or imperial (lb, in, lb-in) in one click. Visitors from the US get imperial units automatically. Worked example from the video (also in the guide on the page): 50 kg carriage, Ø25 mm ball screw with 20 mm lead, 300 mm in 0.6 s with a 1/3 trapezoid profile. Load inertia 8.08 kg·cm², motor speed 2250 rpm. A low-inertia 0.4 kW motor has enough torque, but its inertia ratio is 33; a medium-inertia 0.75 kW motor brings it down to 4.9. On this axis the inertia ratio, not the torque, decides the motor. The page also has the formulas, a step-by-step guide and an FAQ, so you can check every result by hand. More free engineering calculators: https://www.onxcontrol.com/en/calculators ONX Control, Istanbul: motion control, automation and servo systems. #servomotor #motioncontrol #automation

30 saniyede servo motor seçimi (ücretsiz hesaplama) #shorts
Ücretsiz motor boyutlandırma aracı: tepe ve RMS tork, atalet oranı ve uygun servo motor. Metrik ya da inç-pound. onxcontrol.com → Hesaplamalar → Motor boyutlandırma #servomotor #otomasyon #mühendislik #shorts

Size a servo motor in 30 seconds (free calculator) #shorts
Free servo motor sizing calculator: peak and RMS torque, inertia ratio and matching servo motors. Metric or imperial. onxcontrol.com → Calculators → Motor sizing #servomotor #engineering #automation #shorts

Onx CNC RTCP – 5 eksen takım ucu kontrolü (Tool Center Point), CODESYS RTE'de canlı
X CNC Library ve Onx CNC Web HMI ile RTCP (Rotational Tool Center Point). Programda M140 ile RTCP açılır; X Y Z artık kafanın değil takım ucunun konumudur. A/C kafa dönerken kontrolör X Y Z'yi gerçek zamanlı düzelterek takım ucunu programlanan yolda tutar; F takım ucunun hızıdır. CODESYS Control RTE, 1 ms interpolasyon, look-ahead ve jerk sınırlı planlama, sanal eksenler. Kinematik: A/C çatallı kafa, pivot–uç 150 mm. Videoda (rtcp_rte1.cnc): 0:00 Giriş, Start ve M140 (RTCP açık) 0:10 Yalnız yönelim: A 30° ve C 360°, takım ucu sabit 0:23 Takım eğilirken uç düz çizgide, eğik takımla yay (G2) 0:37 Yönelim değişen G0 ve 3+2 (A −45°) dalış 0:53 C 180° dönerken uç düz çizgide, M141 ile makine koordinatlarına dönüş RTCP on CODESYS Control RTE with the X CNC Library and the Onx CNC web HMI: with M140 the program describes the tool tip and the controller compensates X Y Z in real time while the A/C head rotates. 1 ms interpolation, look-ahead, jerk-limited planning, virtual axes. Müzik: bu video için özgün olarak üretildi. / Music: original, made for this video. #CNC #RTCP #CODESYS

CODESYS EtherCAT Portunu Windows Güncellemelerine Karşı Kilitleme | Nexcom IPC · CODESYS RTE
Windows Update veya otomatik sürücü arama, CODESYS RTE sürücüsü kurulu EtherCAT portunun sürücüsünü standart Intel/Microsoft sürücüsüyle değiştirebilir. Bu durumda EtherCAT haberleşmesi kesilir ve makine durur. Bu videoda ONX Control olarak geliştirdiğimiz dört katmanlı koruma çözümünü anlatıyoruz: 1) Port kilidi: EtherCAT portunun sürücü kurulumu sistem ilkesiyle engellenir 2) Windows Update üzerinden sürücü dağıtımı kapatılır (güvenlik güncellemeleri devam eder) 3) LTSC olmayan sürümlerde Windows sürümü sabitlenir 4) Açılış bekçisi: sürücü doğrulanmadan CODESYS servisleri başlatılmaz, sonuç ekranda gösterilir Desteklenen sistemler: Windows 10 / 11 (LTSB, LTSC, IoT Enterprise, Pro, Enterprise) · CODESYS Control RTE V3 · Nexcom ve benzeri çift Intel I210 portlu endüstriyel PC'ler Script ve kurulum desteği için: https://www.onxcontrol.com BÖLÜMLER 0:00 Giriş 0:23 Sorun 0:57 Çözüm 1:35 Kurulum 2:54 Doğrulama 4:49 Bakım 5:27 Notlar ENGLISH Windows Update can silently replace the CODESYS RTE driver on your EtherCAT port and stop the machine. This video shows ONX Control's four-layer protection: port driver lock, no drivers via Windows Update, version pinning and a boot guard that starts CODESYS only after the driver is verified. English subtitles available. #CODESYS #EtherCAT #EndüstriyelOtomasyon

ONX Control Company Introduction | PC-Based Automation, Servo and Motion Control
Since 2013, ONX Control (Oniks Kontrol Sistemleri) has delivered PC-based automation, servo and motion control solutions to machine builders from Istanbul: control system design, machine software, control panels, field commissioning and retrofit. Every machine in this video is a real field application automated by ONX Control. 0:00 ONX Control: who we are 0:20 Metal lines: flying shears, rotary knives, tube bending 0:34 Packaging and food 0:47 Cable extrusion and textile 0:57 Tissue and paper 1:08 CNC and window machines 1:18 Our own software: X CNC Library, CODESYS, EtherCAT 1:30 Official partnerships and 18 countries 1:43 Services Official partnerships: CODESYS System Partner · Nidec Drives (Control Techniques) distributor and system integrator · ESTUN authorized distributor · CREVIS distributor for Türkiye · NEXCOM channel partner · Leroy-Somer authorized dealer Solutions: https://www.onxcontrol.com/en/solutions Contact: +90 216 504 14 42 · info@onxcontrol.com #ONXControl #Automation #Servo #CODESYS #MotionControl

ONX Control Kurumsal Tanıtım | PC Tabanlı Otomasyon, Servo ve Hareket Kontrolü
ONX Control (Oniks Kontrol Sistemleri), 2013'ten bu yana İstanbul'dan makine üreticilerine PC tabanlı otomasyon, servo ve hareket kontrolü çözümleri sunuyor: kontrol sistemi tasarımı, makine yazılımı, otomasyon panosu, saha devreye alma ve retrofit. Bu videodaki tüm makineler ONX Control'ün otomasyonunu yaptığı gerçek saha uygulamalarıdır. 0:00 ONX Control: biz kimiz 0:20 Metal hatları: uçar makas, döner bıçak, boru bükme 0:34 Paketleme ve gıda 0:47 Kablo ekstrüzyonu ve tekstil 0:57 Tissue ve kağıt 1:08 CNC ve doğrama 1:18 Kendi yazılımımız: X CNC Library, CODESYS, EtherCAT 1:30 Resmi iş ortaklıkları ve 18 ülke 1:43 Hizmetler Resmi iş ortaklıkları: CODESYS System Partner · Nidec Drives (Control Techniques) distribütör ve sistem entegratörü · ESTUN yetkili distribütör · CREVIS Türkiye distribütörü · NEXCOM kanal partneri · Leroy-Somer yetkili bayi Çözümler: https://www.onxcontrol.com/cozumler Kurumsal: https://www.onxcontrol.com/kurumsal İletişim: +90 216 504 14 42 · info@onxcontrol.com #ONXControl #Otomasyon #ServoMotor #CODESYS #HareketKontrolü

5 eksen türbin, 139.882 satır G-code: canlı 3B yol ve 1 ms trace #shorts
X CNC Library ve Onx CNC Web HMI ile 5 eksenli türbin programı CODESYS Control RTE'de canlı: 3B yol, A/C'den takım ekseni, anlık override ile hız/ivme/jerk, yolu renklendirme, 1 ms trace. Tam video: https://youtu.be/zU6QiOHeIQ4

Onx CNC Web HMI – 5 eksen türbin, 139.882 satır G-code, CODESYS RTE'de canlı
X CNC Library ve Onx CNC Web HMI ile 5 eksenli (X Y Z A C) türbin rozeti programının canlı çalışması. CODESYS Control RTE, 1 ms interpolasyon, look-ahead planlama, sanal eksenler. Videoda: işi tek tıkla başlatma ve canlı iş durumu, gerçek zamanlı 3B yol görünümü (program, işlenen kısım, komut ve gerçek yol), A/C'den takım ekseni, çalışırken override (hız/ivme/jerk grafikleri), yolu C ekseni veya F'ye göre renklendirme, 1 ms canlı trace, dahili G-code editörü, eksen limitleri (iş boyunca min/max). Live 5-axis turbine rosette job on CODESYS Control RTE with the X CNC Library and the Onx CNC web HMI.

Makineyi biz yönetiyoruz: PC tabanlı otomasyon #shorts
ONX Control 2013'ten bu yana İstanbul'dan makine üreticilerine PC tabanlı otomasyon, servo ve hareket kontrolü sunuyor: kontrol sistemi tasarımı, makine yazılımı, otomasyon panosu ve saha devreye alma. Videodaki tüm makineler gerçek saha uygulamalarımız. Kurumsal tanıtım videosu: https://youtu.be/hSPz7BReE1k Çözümler: https://www.onxcontrol.com/cozumler #ONXControl #Otomasyon #ServoMotor #CODESYS #HareketKontrolü

Panel kesimde milimetrik yol: CNC router kontrolü #shorts
ONX Control'ün kontrol sistemini kurduğu CNC router'lar: MDF ve mobilya paneli kesimi, menteşe delikleri. G-kodu ve look-ahead hız planı X CNC Library ile, kontrol endüstriyel PC üzerinde CODESYS Control RTE ile, eksenler EtherCAT servo sürücülerle çalışır. Çözümler: https://www.onxcontrol.com/cozumler #ONXControl #CNCRouter #Otomasyon #EtherCAT #CODESYS

Kağıt hiç durmuyor: non-stop tissue sarma hattı #shorts
ONX Control'ün kontrolünü yaptığı tissue (havlu ve tuvalet kağıdı) sarma hattından Kenya saha görüntüleri: ana bobin açıcı, non-stop sarıcıda hat durmadan yeni masuraya geçiş, masura makinesi ve log biriktirme. Kontrol CODESYS ile. Çözümler: https://www.onxcontrol.com/cozumler #ONXControl #Tissue #Otomasyon #ServoMotor #CODESYS

Bıçak dönüyor, sac durmuyor: döner bıçakla boy kesim #shorts
ONX Control'ün otomasyonunu yaptığı gerçek saha uygulamaları: döner bıçaklı boy kesim. Bıçak sacın hızına senkron döner, sac hiç durmadan istenen boyda kesilir. Çift motorlu döner makas (hareket analiziyle ayarlandı), 2 mm rotary boy kesim hattı ve 80 m/dk etiket kesim. Çözümler: https://www.onxcontrol.com/cozumler #ONXControl #RotaryKnife #Otomasyon #ServoMotor #CODESYS

Hat durmadan kesiyor: uçar makas, servo senkron #shorts
ONX Control'ün otomasyonunu yaptığı gerçek saha uygulaması: uçar makas. Profil ve boru hattı durmadan akarken kesim tarafı kesim anında hatla aynı hıza çıkar, keser ve geri döner. Çift kafa, CODESYS SoftMotion, servo senkron. Çözümler: https://www.onxcontrol.com/cozumler #ONXControl #UçarMakas #Otomasyon #ServoMotor #CODESYS

Tissue Converting Line: Non-Stop Rewinder, Log Saw and Core Maker (Kenya) | ONX Control
Field footage from Kenya of a tissue (toilet and kitchen towel) converting line controlled by ONX Control: parent roll unwinder, servo perforation, change to a new core on the non-stop rewinder, core maker and log accumulator. - Control: CODESYS, virtual master axis and perforation sync - The tear moment is calculated from sheet count and perforation angle, so the paper tears at the perforation line every time - EtherCAT, Crevis I/O, multilingual operator screen Tissue converting line automation: https://www.onxcontrol.com/en/solutions/tissue-converting-line-automation #ONXControl #Tissue #PaperConverting #LogSaw #Automation

Tissue Sarma Hattı: Non-Stop Sarıcı, Log Saw ve Masura Makinesi (Kenya) | ONX Control
ONX Control'ün kontrolünü yaptığı tissue (havlu ve tuvalet kağıdı) sarma hattından Kenya saha görüntüleri: ana bobin açıcı, servo perforasyon, non-stop sarıcıda yeni masuraya geçiş, masura makinesi ve log biriktirme. - Kontrol: CODESYS, sanal ana eksen ve perfore senkronu - Koparma anı yaprak sayısı ve perfore açısıyla hesaplanır; kağıt her seferinde perfore hattından kopar - EtherCAT, Crevis I/O, çok dilli operatör ekranı Havlu ve tuvalet kağıdı sarma hattı otomasyonu: https://www.onxcontrol.com/cozumler/havlu-tuvalet-kagidi-sarma-hatti-otomasyonu #ONXControl #Tissue #KağıtSarma #LogSaw #Otomasyon

CNC Router Control System: Furniture Panels, Composites and MDF | ONX Control
Field footage from CNC routers controlled by ONX Control: MDF and furniture panel cutting, composite contours and hinge holes. - G-code, look-ahead velocity planning and tool compensation: X CNC Library - Control: CODESYS Control RTE on an industrial PC - X, Y1, Y2 and Z axes: EtherCAT servo drives - Operator interface: 3D simulation, vacuum zoning, estimated finish time CNC router control system: https://www.onxcontrol.com/en/solutions/cnc-router-control-system X CNC Library: https://www.onxcontrol.com/en/products/x-cnc #ONXControl #CNCRouter #CODESYS #Furniture #EtherCAT

CNC Router Kontrol Sistemi: Mobilya Paneli, Kompozit ve MDF Kesim | ONX Control
ONX Control'ün kontrol sistemini kurduğu CNC router'lardan saha görüntüleri: MDF ve mobilya paneli kesimi, kompozit kontur, menteşe delikleri. - G-kodu, look-ahead hız planı ve takım telafisi: X CNC Library - Kontrol: endüstriyel PC üzerinde CODESYS Control RTE - X, Y1, Y2 ve Z eksenleri: EtherCAT servo sürücüler - Operatör arayüzü: 3D simülasyon, vakum bölgeleme, tahmini bitiş süresi CNC router kontrol sistemi: https://www.onxcontrol.com/cozumler/cnc-router-kontrol-sistemi X CNC Library: https://www.onxcontrol.com/urunler/x-cnc #ONXControl #CNCRouter #CODESYS #Mobilya #EtherCAT

Otomatik cep takma: katla, dik, istifle #shorts
Otomatik cep takma makinesi: cep kalıpla katlanır, X-Y servo eksenlerle dikilir, otomatik istiflenir. CODESYS, Estun ED3L EtherCAT servo, Crevis I/O. Otomatik cep takma ve dikiş otomasyonu: https://www.onxcontrol.com/cozumler/otomatik-cep-takma-dikis-makinesi-otomasyonu Uzun sürüm: https://youtu.be/6bLpXGLFym0 #ONXControl #CepTakma #DikişOtomasyonu

Automatic Pocket Setter: X-Y Servo Sewing and Mould Folding | ONX Control
A bathrobe pocket on an automatic pocket setter: the operator places the pocket on the mould, the mould folds it and carries it to the panel, the sewing head follows the stitch path with X-Y servo axes in sync with the needle, and the finished part is stacked automatically. - Control: CODESYS on an industrial PC - X-Y stitch axes: Estun ED3L EtherCAT servo drives - Folding, mould and stacking: Crevis EtherCAT I/O - Operator interface: panel PC Since 2021 ONX Control has done the control of back pocket, coin pocket, bellows pocket, kangaroo pocket, bathrobe pocket, belt and J-stitch machines. Automatic pocket setter and sewing automation: https://www.onxcontrol.com/en/solutions/automatic-pocket-setter-sewing-automation #ONXControl #PocketSetter #SewingAutomation #Garment #Servo
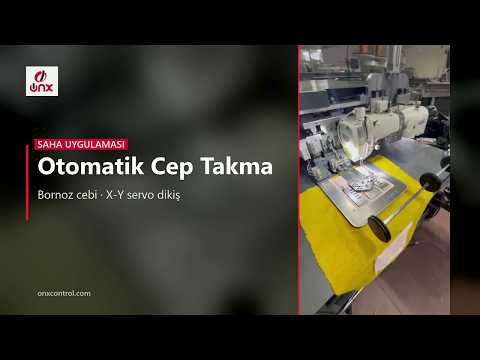
Otomatik Cep Takma Makinesi: X-Y Servo Dikiş ve Kalıpla Katlama | ONX Control
Otomatik cep takma makinesinde bornoz cebi uygulaması: operatör cebi kalıba koyar, kalıp cebi katlayıp panele taşır, dikiş kafası X-Y servo eksenlerle dikiş yolunu iğneye senkron izler, dikilen parça otomatik istiflenir. - Kontrol: endüstriyel PC üzerinde CODESYS - X-Y dikiş eksenleri: Estun ED3L EtherCAT servo sürücüler - Katlama, kalıp ve istifleme: Crevis EtherCAT I/O - Operatör arayüzü: panel PC ONX Control 2021'den bu yana arka cep, çakmak cep, körüklü cep, kanguru cep, bornoz cebi, kemer ve J dikiş makinelerinin kontrolünü yapıyor. Otomatik cep takma ve dikiş otomasyonu: https://www.onxcontrol.com/cozumler/otomatik-cep-takma-dikis-makinesi-otomasyonu #ONXControl #CepTakma #DikişOtomasyonu #Konfeksiyon #ServoMotor
17 eksen servo, dakikada 600+ kek paketi #shorts
ONX Control'ün otomasyonunu yaptığı 17 eksen servo kontrollü kek paketleme hattı: akıllı bant, asker zinciri, yatay paketleme makinesi. Akıllı bant nasıl çalışır: https://www.onxcontrol.com/cozumler/akilli-bant-otomasyonu Uzun sürüm: https://youtu.be/lbkOOMVtieE #ONXControl #AkıllıBant #PaketlemeOtomasyonu

17-Axis Servo Cake Packaging Line: Smart Belt and Lug Chain | ONX Control
A 17-axis servo cake packaging line automated by ONX Control, in 36 seconds. Randomly spaced cakes are buffered on an accumulation belt; the smart belt detects every product with a photo-eye, gaps it and puts it in phase with the packaging machine's master axis. A lug chain transfers the cakes to the horizontal flow wrapper in sync; print registration is corrected on every pack and the rotary jaws seal and cut. Machine speed is shown live on the operator panel: more than 600 packs per minute. - 17 servo axes, one master axis - Control Techniques servo drives - Film speed up to 70 m/min How a smart belt works: https://www.onxcontrol.com/en/solutions/smart-belt-intelligent-infeed Product phasing into a lug chain: https://www.onxcontrol.com/en/solutions/product-phasing-lug-chain-infeed Horizontal flow wrapper automation: https://www.onxcontrol.com/en/solutions/horizontal-flow-wrapper-automation #ONXControl #SmartBelt #PackagingAutomation #Servo #FlowWrapper

17 Eksen Servo Kek Paketleme Hattı: Akıllı Bant ve Asker Zinciri | ONX Control
ONX Control'ün otomasyonunu yaptığı 17 eksen servo kontrollü kek paketleme hattı, 36 saniyede. Düzensiz gelen kekler biriktirme bandında toplanır; akıllı bant her ürünü fotoselle ölçer, aralar ve paketleme makinesinin ana eksenine göre faza oturtur. Kekler asker zinciriyle yatay paketleme makinesine senkron aktarılır; folyo baskı izi fotoselle her pakette düzeltilir, döner çene paketi kapatıp keser. Makina hızı operatör panelinden canlı izlenir: dakikada 600'ü aşan paket. - 17 servo eksen, tek ana eksen - Control Techniques servo sürücüler - Folyo hızı 70 m/dk'ya kadar Akıllı bant nasıl çalışır: https://www.onxcontrol.com/cozumler/akilli-bant-otomasyonu Asker zincirine ürün fazlama: https://www.onxcontrol.com/cozumler/asker-zinciri-urun-faz-senkronizasyonu Yatay paketleme makinesi otomasyonu: https://www.onxcontrol.com/cozumler/yatay-paketleme-makinesi-otomasyonu Uzun saha videosu: https://www.youtube.com/watch?v=-eGjJiMLj6k #ONXControl #AkıllıBant #PaketlemeOtomasyonu #ServoMotor #Ambalaj

5 Eksen CNC Testi: Çiçek Madalyonu | X CNC Library – CODESYS | Onx Control
ONX X CNC Library, zorlu bir 5 eksen (X Y Z A C) test programını CODESYS Control RTE üzerinde çalıştırıyor; görüntü Onx CNC web HMI yol görünümünden, gerçek hızda. Programda neler var: • Çerçeve: 640 mm uzun doğrular, R40 yaylar ve 45° pahlar (135° köşeler) • XZ (G18) ve YZ (G19) düzleminde kemerler • Takım eğiminin (A) eğimi izlediği dalga saçak – 4 eksen birlikte • 0,6 mm adıma inen elmas zikzak – 180°'ye yakın ters dönüşler • 0,1 mm mikro parçalı dalgalı halka • Helis yaylı, sivri uçlu yapraklar ve helis perçinler • 8 yapraklı gül: takım her yaprağa eğik, A = 0 kutbundan geçerken C 180° döner • 24 meridyenli kubbe: kutupta saf C dönüşü, takım küre normalinde Tüm eksenler hız, ivme ve jerk limitleri içinde kalır. --- The ONX X CNC Library runs a demanding 5-axis (X Y Z A C) test program on CODESYS Control RTE, shown live in the Onx CNC web HMI path view, in real time: long lines, arcs and chamfers, G18/G19 arches, a 4-axis wave border, a diamond zigzag down to 0.6 mm steps, a ripple ring with 0.1 mm micro segments, helical leaves and rivets, an 8-petal rose passing the A = 0 pole (C turns 180°) and a dome with 24 meridians. Every axis stays within its velocity, acceleration and jerk limits. Onx Control Systems and Engineering – www.onxcontrol.com #CNC #5eksen #5axis #CODESYS #OnxControl

X_CNC Web Visu
Bu videoda, ONX X CNC Library fonksiyon blokları (X_CNC) ile çalışan bir CODESYS Web Visu örneği gösterilmektedir. X CNC Library; G-code okuma ve yorumlamadan sonra yol yumuşatma (G51 köşe yuvarlama), jerk sınırlı hız profili ve 5 eksene kadar (X Y Z A C) interpolasyon sağlayan, CODESYS SoftMotion'a alternatif bir CNC kütüphanesidir. Web Visu sayesinde makine; bilgisayar, tablet veya telefon tarayıcısından izlenip kullanılabilir. Örnekte program seçimi, çalıştırma ve yol takibi gibi temel CNC işlevleri görülmektedir. English: A CODESYS Web Visu example running with the ONX X CNC Library function blocks (path smoothing, jerk-limited velocity planning, up to 5-axis interpolation). ONX Control – Oniks Kontrol Sistemleri: endüstriyel otomasyon, servo ve motion control, CNC, CODESYS ve EtherCAT çözümleri. Web: www.onxcontrol.com #ONXControl #Otomasyon #Automation #MotionControl #CNC #CODESYS #WebVisu

Kanguru Cep Takma Makinası | CODESYS CNC Kontrol ve Kalınlık Algoritması
Bu uygulamada, kanguru cep üretimi için geliştirilen özel makine otomasyonu gösterilmektedir. Sistem; CNC kontrollü hareket yapısı, özel kalınlık kontrol algoritması ve hassas proses yönetimi ile tekrarlanabilir ve hatasız üretim hedefiyle tasarlanmıştır. ONX Control mühendislik yaklaşımıyla geliştirilen çözüm; makine hareketlerinin senkron kontrolü, operatör kullanım kolaylığı ve üretim kalitesinin sürdürülebilirliği üzerine kurgulanmıştır. Bu video, özel amaçlı tekstil ve dikiş makinesi otomasyonlarında CODESYS tabanlı kontrol mimarisinin nasıl uygulanabileceğine dair bir saha referansıdır.

4 Kafa PVC Kaynak ve CNC Köşe Temizleme Hattı | ONX Control Otomasyon Referansı
Bu videoda, dört kafa PVC kaynak ve CNC köşe temizleme hattına ait otomasyon uygulaması gösterilmektedir. Sistem; PVC profil kaynak işlemi, robotik/otomatik taşıma akışı ve CNC köşe temizleme operasyonlarını tek üretim hattı üzerinde entegre edecek şekilde tasarlanmıştır. ONX Control tarafından geliştirilen otomasyon mimarisi; hat senkronizasyonu, hareket kontrolü, operatör arayüzü ve üretim çevriminin güvenilir şekilde yönetilmesine odaklanır. Bu uygulama, PVC pencere ve profil üretim hatlarında yüksek verimlilik, proses tekrarlanabilirliği ve otomasyon standardizasyonu için geliştirilmiş bir saha referansıdır.

Rotary Shear / Döner Makas Kontrolü | CODESYS RTE ve EtherCAT Senkronizasyon
Bu uygulama, ONX Control tarafından geliştirilen CODESYS RTE tabanlı rotary shear / döner makas kontrol çözümünü göstermektedir. Sistemde döner makas mekanizması iki ayrı servo motor ve iki ayrı sürücü ile kontrol edilmekte, eksenler arası senkronizasyon EtherCAT tabanlı mimari üzerinden sağlanmaktadır. Uygulamada ONX Motion kütüphanesi kullanılarak yüksek hızlı kesim çevrimlerinde pozisyon, hız ve senkron hareket kontrolü gerçekleştirilmiştir. Bu yapı; ambalaj, folyo, kağıt, karton ve benzeri sürekli hat uygulamalarında hassas kesim ve tekrarlanabilir proses kontrolü için uygundur. Bu video, CODESYS RTE, EtherCAT ve motion control teknolojilerinin gerçek bir saha uygulamasındaki kullanımını gösteren ONX Control mühendislik referansıdır.

Karton Kutu Makinası Otomasyonu | ONX Control Saha Uygulaması
Bu videoda, karton kutu üretim veya kutu işleme prosesine yönelik makine otomasyonu uygulaması gösterilmektedir. Sistem; makine çevriminin kontrolü, hareketlerin senkron yönetimi, operatör arayüzü ve üretim sürekliliği dikkate alınarak yapılandırılmıştır. ONX Control mühendislik ekibi tarafından geliştirilen otomasyon yaklaşımı; servo sürücüler, PLC/SoftPLC kontrol, sensör geri bildirimleri ve proses güvenliği gibi endüstriyel otomasyon bileşenlerini bir araya getirir. Bu çalışma, ambalaj makineleri ve karton işleme hatları için geliştirilen saha otomasyon referanslarından biridir.

Rotary Shear 15 mm | Hassas Döner Makas Kontrolü
Bu uygulama, 15 mm kesim hassasiyetine yönelik rotary shear / döner makas kontrol sistemini göstermektedir. Makine hareketleri, kesim prosesiyle senkron çalışacak şekilde kontrol edilerek yüksek hızda tekrarlanabilir kesim performansı hedeflenmiştir. ONX Control tarafından geliştirilen çözüm; servo eksen kontrolü, senkron hareket yönetimi ve endüstriyel haberleşme altyapısıyla döner bıçak/döner makas uygulamaları için esnek bir otomasyon mimarisi sunar. Bu video, ambalaj ve sürekli hat uygulamalarında kullanılan hassas kesim çözümleri için ONX Control saha referansıdır.

ONX Control Kurumsal Tanıtım | Endüstriyel Otomasyon ve Makine Kontrol Sistemleri
ONX Control; endüstriyel otomasyon, sürücü sistemleri, servo kontrol, PC tabanlı kontrol, CODESYS Runtime, EtherCAT, Motion Control, CNC ve makine otomasyonu alanlarında mühendislik çözümleri geliştiren bir otomasyon firmasıdır. Bu tanıtım videosunda ONX Control’ün saha uygulamaları, mühendislik yaklaşımı ve makine imalatçılarına sunduğu otomasyon çözümleri genel hatlarıyla gösterilmektedir. ONX Control; standart PLC uygulamalarından yüksek eksenli motion ve CNC projelerine kadar geniş bir alanda, projeye özel kontrol mimarileri ve saha devreye alma desteği sunar.

Rotary Knife Otomasyonu | ONX Control Servo Senkronizasyon Uygulaması
Bu videoda, ONX Control tarafından otomasyonu gerçekleştirilen rotary knife / döner bıçak uygulaması gösterilmektedir. Sistem, sürekli hareket eden ürün veya malzeme akışı üzerinde hassas kesim yapabilmek için servo eksenlerin senkron kontrolüne dayanır. Rotary knife uygulamaları; kesim uzunluğu, hat hızı, ürün senkronizasyonu ve bıçak çevriminin doğru yönetilmesini gerektirir. ONX Control çözümü, bu gereksinimleri karşılamak üzere hareket kontrolü ve endüstriyel otomasyon bileşenlerini bir araya getirir. Bu uygulama; ambalaj, folyo, kağıt, karton ve benzeri sürekli üretim hatları için geliştirilmiş bir motion control referansıdır.

ONXCONTROL COMMERCIAL
Oniks Kontrol (ONX Control) tanıtım filmi. ONX Control; makine imalatçılarına yönelik endüstriyel otomasyon, servo ve motion control, CNC ve PC tabanlı kontrol (CODESYS Runtime, EtherCAT) çözümleri geliştirir. Videoda farklı sektörlerde devreye aldığımız makinelerden kesitler yer almaktadır: kesim ve uçar makas hatları, CNC uygulamaları, ambalaj ve özel amaçlı makineler. Yazılım geliştirme, sürücü seçimi, pano ve saha devreye alma dahil olmak üzere, makinenin fikir aşamasından üretime kadar mühendislik desteği sunuyoruz. English: Company film of Oniks Kontrol (ONX Control) – industrial automation, servo and motion control, CNC and PC-based control (CODESYS, EtherCAT) for machine builders. ONX Control – Oniks Kontrol Sistemleri: endüstriyel otomasyon, servo ve motion control, CNC, CODESYS ve EtherCAT çözümleri. Web: www.onxcontrol.com #ONXControl #Otomasyon #Automation #MotionControl #CODESYS #EtherCAT

ESTUN ED3L Servo Sürücü Tanıtımı | ONX Control
Bu videoda ESTUN ED3L servo sürücü ailesine yönelik genel tanıtım ve uygulama yaklaşımı gösterilmektedir. Servo sürücüler; hassas pozisyonlama, hız kontrolü, tork kontrolü ve makine hareketlerinin dinamik şekilde yönetilmesi için endüstriyel otomasyon sistemlerinde kritik bir rol üstlenir. ONX Control, servo sürücü seçimi, devreye alma, haberleşme entegrasyonu, motion control uygulamaları ve makine yazılımı geliştirme konularında mühendislik desteği sunar. Bu video, servo kontrollü makine otomasyonlarında ED3L sürücülerin kullanımına yönelik genel bir tanıtım içeriğidir.

PLC Programming Learn the basics with CoDeSys 2
CODESYS ile PLC programlamaya giriş serisinin 2. bölümü. Bu bölümde ilk bölümde oluşturulan proje üzerinde örnek bir program yazılması, derlenmesi ve simülasyonda / kontrolcüde çalıştırılıp izlenmesi gösterilmektedir. English: Part 2 of the CODESYS PLC programming basics – writing, compiling and running / monitoring a first program. ONX Control – Oniks Kontrol Sistemleri: endüstriyel otomasyon, servo ve motion control, CNC, CODESYS ve EtherCAT çözümleri. Web: www.onxcontrol.com #ONXControl #Otomasyon #Automation #CODESYS #PLC #IEC61131

PLC Programming Learn the basics with CoDeSys 1
CODESYS ile PLC programlamaya giriş serisinin 1. bölümü. Bu bölümde CODESYS geliştirme ortamı ve yeni bir projenin oluşturulmasından başlayarak PLC programlamanın temel adımları gösterilmektedir. Seri; IEC 61131-3 dilleriyle (ST, LD vb.) PLC programlamaya yeni başlayanlar ve CODESYS tabanlı kontrolcülerle çalışmak isteyen mühendisler için hazırlanmıştır. English: Part 1 of an introduction to PLC programming with CODESYS – the development environment and the first steps of a new project. ONX Control – Oniks Kontrol Sistemleri: endüstriyel otomasyon, servo ve motion control, CNC, CODESYS ve EtherCAT çözümleri. Web: www.onxcontrol.com #ONXControl #Otomasyon #Automation #CODESYS #PLC #IEC61131

Fram Cutting Machine
CODESYS SoftMotion CNC tabanlı çerçeve (frame) kesim makinesi. Kesim eksenleri, CNC yol hareketi ve makine çevrimi CODESYS altyapısında tek yazılım mimarisiyle yönetilmektedir. Aynı makinenin ayrıntılı anlatımı kanalımızdaki "Frame Cutting Machine | CODESYS SoftMotion CNC Tabanlı Kesim Otomasyonu" videosundadır. English: Frame cutting machine based on CODESYS SoftMotion CNC – cutting axes, CNC path and machine cycle in one CODESYS project. ONX Control – Oniks Kontrol Sistemleri: endüstriyel otomasyon, servo ve motion control, CNC, CODESYS ve EtherCAT çözümleri. Web: www.onxcontrol.com #ONXControl #Otomasyon #Automation #CNC #CODESYS #SoftMotion

Frame Cutting Machine | CODESYS SoftMotion CNC Tabanlı Kesim Otomasyonu
Bu videoda, CODESYS SoftMotion CNC tabanlı frame cutting machine / çerçeve kesim makinesi otomasyonu gösterilmektedir. Sistem, CNC eksen hareketlerinin kontrolü ve kesim prosesinin hassas şekilde yönetilmesi üzerine kuruludur. CODESYS SoftMotion CNC altyapısı; eksen interpolasyonu, hareket profili yönetimi, pozisyonlama ve makine çevrimi kontrolü gibi fonksiyonları tek yazılım mimarisi altında toplamaya imkân verir. ONX Control tarafından geliştirilen bu tip çözümler; CNC kesim makineleri, özel amaçlı kesim sistemleri ve yüksek hassasiyet gerektiren makine otomasyonları için uygulanabilir.

Double Headed Flying Shear Control | CODESYS SoftMotion CNC Uygulaması
Bu videoda, çift kafalı flying shear / uçan makas kontrol uygulaması gösterilmektedir. Flying shear sistemleri, hareketli malzeme akışı durdurulmadan kesim yapılmasını gerektiren yüksek dinamikli motion control uygulamalarıdır. Uygulama, CODESYS SoftMotion CNC tabanlı kontrol mimarisiyle gerçekleştirilmiştir. Sistem; hat hızı, kesim pozisyonu, eksen senkronizasyonu ve hareket profili yönetimini bir arada ele alır. ONX Control mühendislik çözümü; sürekli üretim hatlarında yüksek hassasiyet, tekrarlanabilir kesim ve verimli çevrim süreleri hedefleyen makine imalatçıları için geliştirilmiştir.

CNC Router | CODESYS SoftMotion CNC Tabanlı Router Kontrolü
Bu videoda, CODESYS SoftMotion CNC tabanlı CNC router uygulaması gösterilmektedir. Sistem; eksen interpolasyonu, takım yolu takibi, pozisyonlama ve makine çevrimi kontrolünü CODESYS altyapısı üzerinden yönetir. CNC router uygulamalarında doğru eksen senkronizasyonu, yumuşak hareket profili, hassas konumlama ve güvenilir operatör kontrolü kritik öneme sahiptir. ONX Control tarafından geliştirilen mimari, bu gereksinimleri endüstriyel otomasyon standardında karşılamayı hedefler. Bu video, CODESYS ile CNC makine kontrolü geliştirmek isteyen üreticiler için gerçek saha uygulaması örneğidir.
Öne Çıkan Motion Uygulamaları
Döner Makas (Rotary Knife)
Salıncak profil (Swing Profile) mimarisi ve ONX Motion Library kullanılarak motor ebatlarını düşüren, sıfır vuruntulu dairesel kesim otomasyonu. Gerçek osiloskop (Trace) eğrileri ve algoritma detayları.
Mühendislik Detayını İnceleUçar Makas (Flying Shear)
CODESYS SoftMotion (PLCOpen) blokları ve EtherCAT kullanılarak profil/boru/sac hatlarında gerçekleştirilen lineer senkronizasyon (CamIn) ve uçan kesim otomasyonu.
Mühendislik Detayını İnceleMimariyi Birlikte Kuralım
ONX Control sistem mühendisleri, üretim hattınıza veya makinenize en uygun CODESYS mimarisini belirlemek için projenizi analiz eder. Teknik detaylar için formu doldurun.
Orijinal Yazılım Şablonları
Motion & CNC Kapasite Analizi
Tam Çevrim Saha Devreye Alma